The Inorganic Chemicals Division is engaged in the development of businesses across the circular economy, including basic inorganic chemical raw materials, detergent ingredients, and water treatment chemicals.

By building specialized supply chains, we aim to deliver new value to our customers and contribute positively to society.

Division Strategy

To achieve stable and sustainable growth, the Inorganic Chemicals Division is strengthening initiatives to develop supply chains for environmentally friendly inorganic chemicals and critical minerals, while advancing the transformation of its business portfolio.

The Division will continue to pursue a dual approach—expanding its core business while driving new business creation—supported by a forward-looking perspective on changes in supply chains and value networks. Building on our core strength in exporting inorganic chemical products from Northeast Asia to Southeast and Southwest Asia, we are creating a reliable framework for stable resource supply.

By responding to evolving customer and societal needs, we aim to maximize competitiveness and identify the most effective strategies to sustain long-term growth.

Strengths of the Division

  • Local Network
    We strengthen our competitiveness
    by collaborating with promising
    partners and leveraging
    the business foundations of our
    group companies.
  • Expansion Capability
    We integrate ideas and capabilities
    to expand our business domains.
  • Long-Established Networks
    and Customer Base
    Our long-established networks and
    customer base enable reliable
    supply, swift market response, and
    consistent value creation.

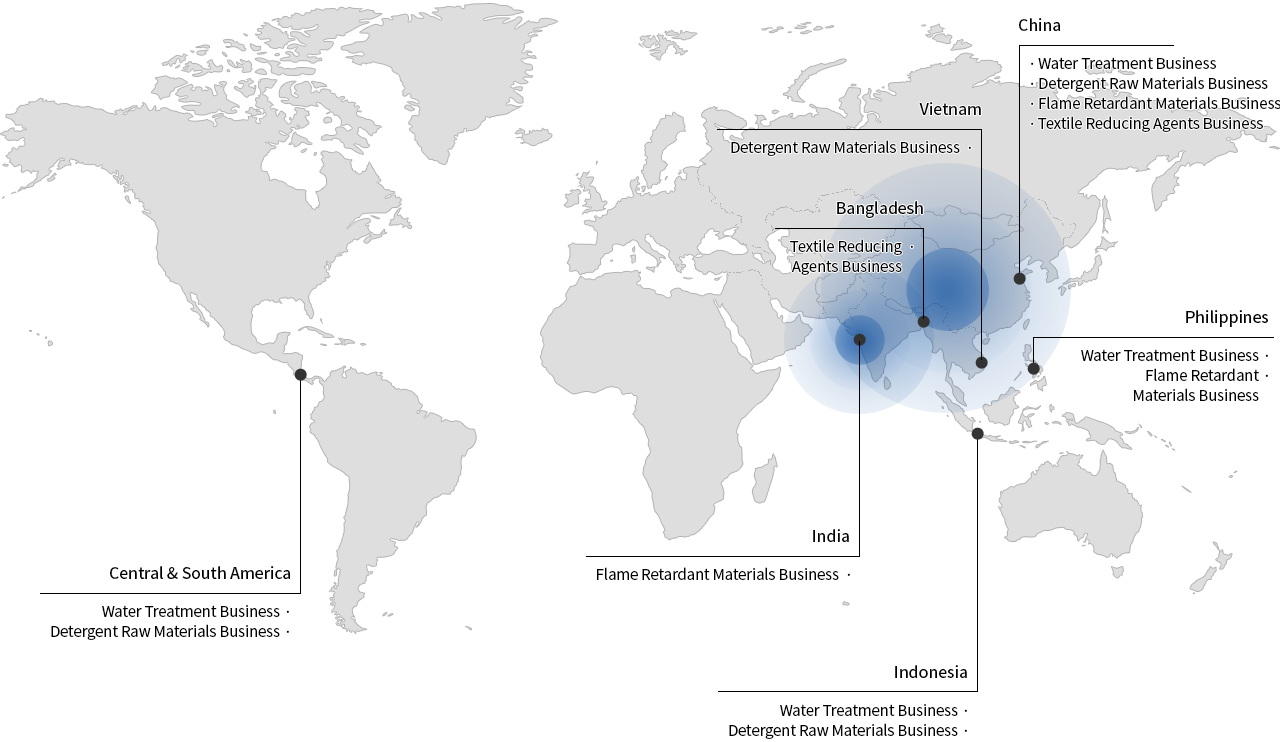
Business Map

Business Overview

  • Water Treatment Business

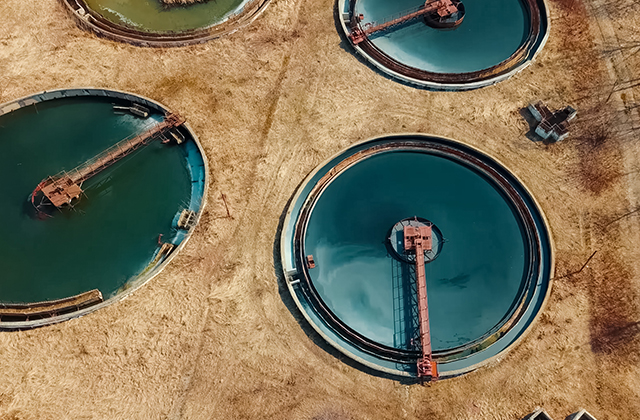
    Leveraging our strong regional network, we supply a wide range of products to customers across Southeast Asia and Southwest Asia.

    We focus on providing stable, high-quality raw materials essential for water purification and wastewater treatment, supporting industries and communities in maintaining safe and sustainable water systems. Through efficient logistics, flexible supply solutions, and close collaboration with our partners, we ensure reliable delivery and consistent value creation.

    By responding to the growing demand for clean water and environmental protection, we are committed to contributing to a more sustainable and resilient future.

  • Detergent Raw Materials Business

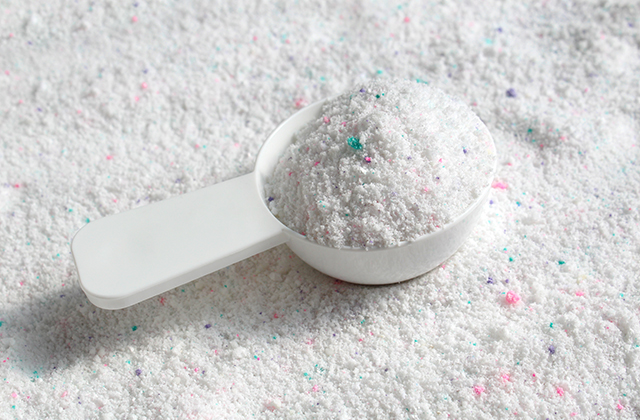
    We supply a comprehensive range of inorganic chemical raw materials used across the detergent industry, covering applications from powdered and liquid detergents to personal care products such as shampoos. Our portfolio supports a wide variety of formulations, enabling customers to meet diverse performance, quality, and cost requirements.

    Through strong sourcing capabilities and established partnerships with leading manufacturers, we ensure consistent quality and a stable supply of key raw materials. In addition, our efficient logistics and flexible delivery solutions allow us to respond quickly to changing market demands.

    By supporting the production of effective and reliable cleaning and personal care products, we contribute to improving everyday life while continuously exploring opportunities aligned with sustainability and evolving industry needs.

  • Flame Retardant Materials Business
    We offer a comprehensive portfolio covering both key raw materials used in the production of flame retardants and a wide range of finished flame retardant products. From foundational inputs to specialized formulations, our solutions support applications in plastics, cables, construction materials, electronics, and other sectors where fire safety is critical.
    Backed by strong sourcing capabilities and close partnerships with leading manufacturers, we ensure consistent quality, technical reliability, and a stable supply of essential materials. Our expertise enables us to provide tailored solutions that meet evolving regulatory requirements and performance standards in global markets. With a focus on safety, innovation, and sustainability, we are committed to supporting our customers in developing high-performance, environmentally responsible products, while contributing to safer living and industrial environments.

Industries We Serve

Supporting essential industries such as water treatment, surface treatment, detergents, construction, and agriculture with dependable inorganic chemical solutions.

Industry Applications
Water Treatment Coagulants, disinfectants, and pH control chemicals play an essential role in municipal and industrial water treatment, supporting water purification, wastewater treatment, and process water management.
Cleaning Chemicals Alkalis, builders, and specialty surfactants are widely used in household and industrial cleaning formulations, contributing to cleaning efficiency, formulation stability, and consistent product performance.
Construction
Materials
Construction additives and mineral-based chemicals are used in cement, concrete, and dry-mix mortar applications to improve workability, strength development, durability, and overall performance.
Rubber & Plastics Mineral fillers, metal oxides, and inorganic additives support rubber and plastic manufacturing by enhancing processing efficiency, mechanical properties, and product consistency.
Textile & Dyeing Bleaching agents, reducing agents, and textile processing chemicals are widely applied in textile pretreatment, dyeing, and finishing processes to achieve consistent quality and efficient production.
Surface Treatment Alkalis, mineral acids, and specialty treatment chemicals are commonly used in metal cleaning, degreasing, pickling, and surface preparation processes prior to coating, plating, and finishing.
Electronics
Manufacturing
Inorganic chemicals such as acids, alkalis, and process chemicals support electronic manufacturing processes, including cleaning, surface preparation, and component production.
Agriculture Fertilizer raw materials, micronutrients, and specialty inorganic chemicals contribute to modern agricultural applications by supporting crop nutrition, soil management, and sustainable farming practices.
Flame Retardant
Materials
Inorganic flame retardant materials, including antimony-based compounds, are widely used in polymers, coatings, textiles, and electronic applications to enhance fire resistance and safety performance.

Organization

Contact Us about Business, Products, or Services
CONTACT top
Asia Alliance
Supporting diverse industries with trusted solutions.
Explore Our Business